
Case Studies
Real projects from our shop floor — how we engineered complete machining solutions around customer parts, machines and cycles.
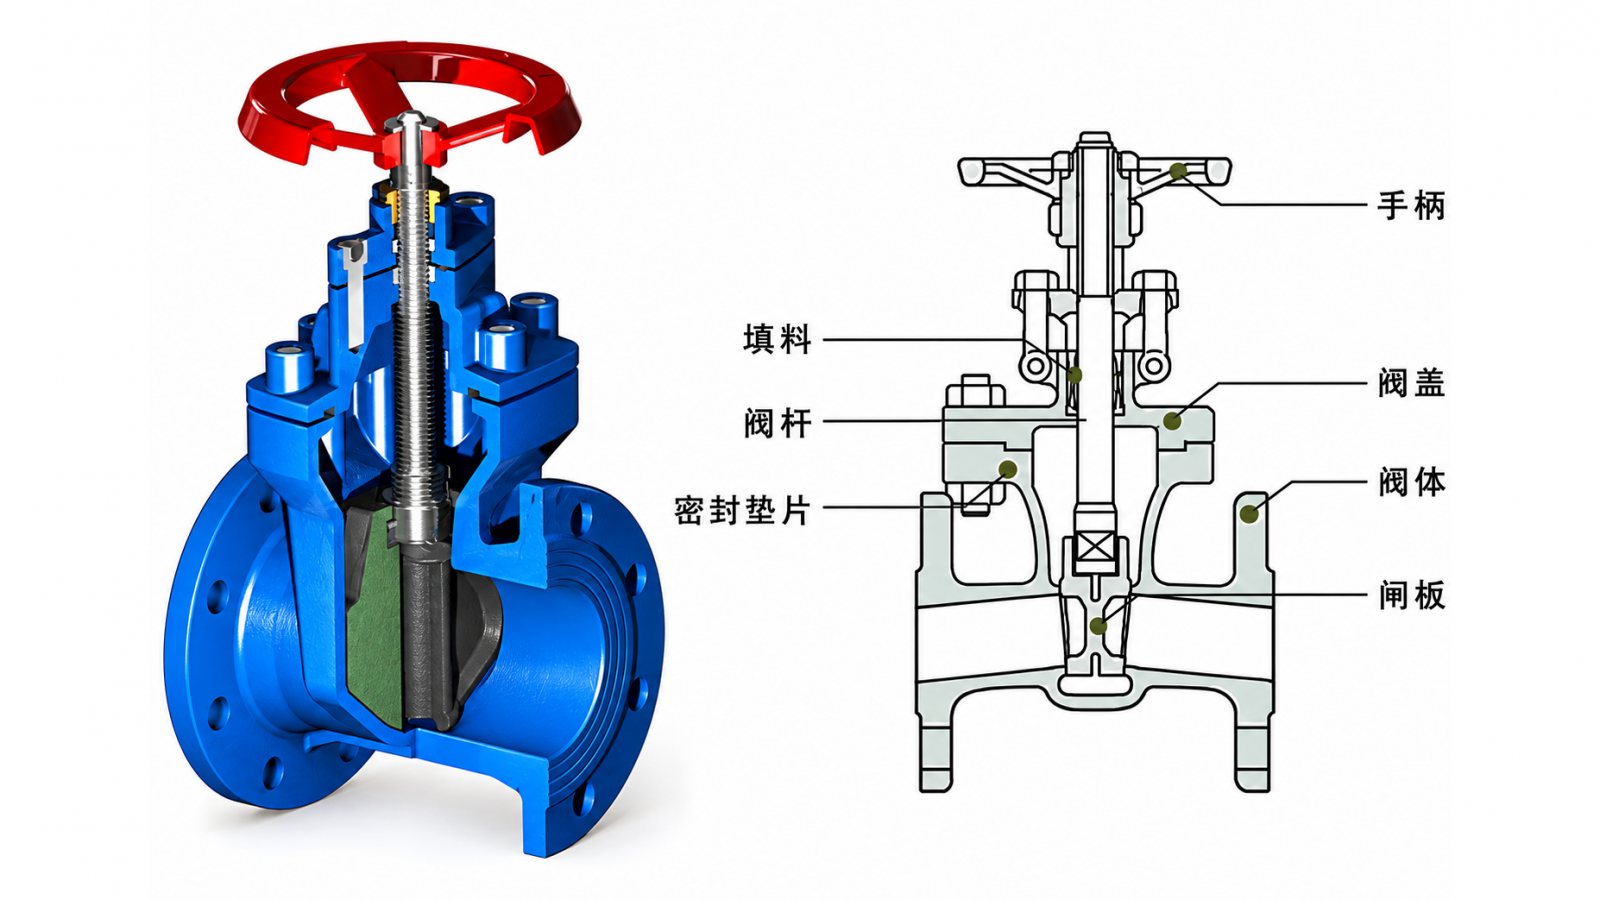
A CNC squaring machine with a dedicated clamping sub-sleeve, spindle taper support and indexable tooling cut the tapered-square cycle on SUS306L gate valve stems from about 3 minutes to 1 minute 20 seconds per piece, with one operator now covering three machines.
Read case study →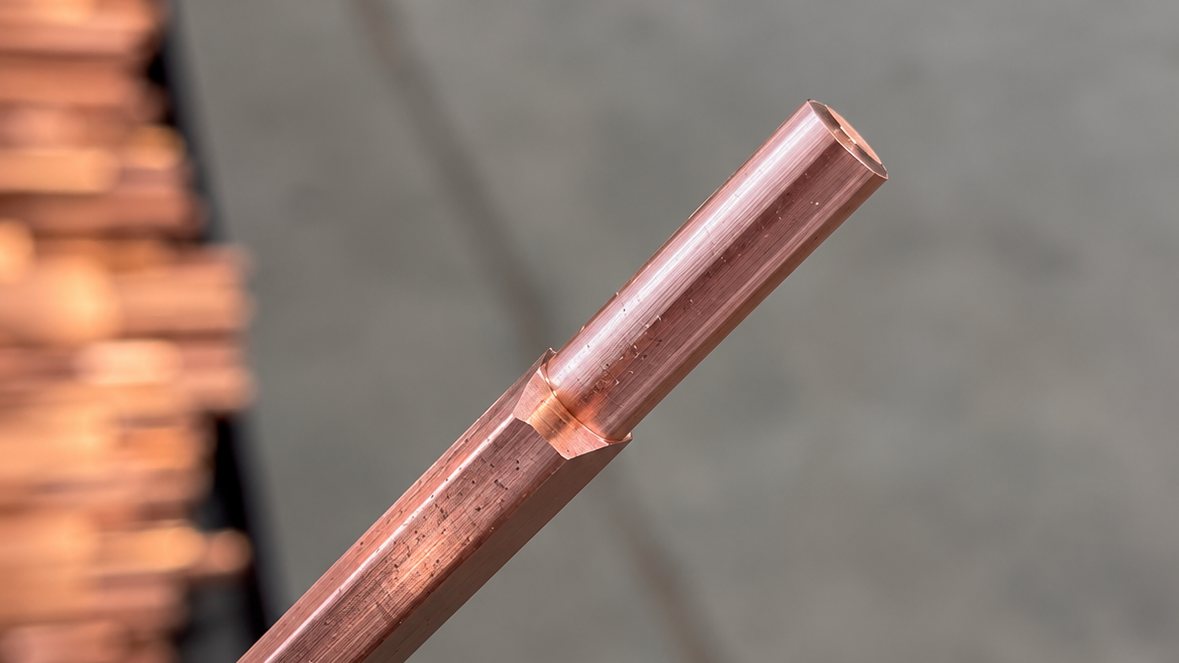
SIPENG CNC developed an automatic CNC turning solution for machining both ends of copper rotor bars used in submersible pump motors. The solution combines dedicated feeding, workholding and internal guidance to improve production output, machining consistency and handling of long copper profiles.
Read case study →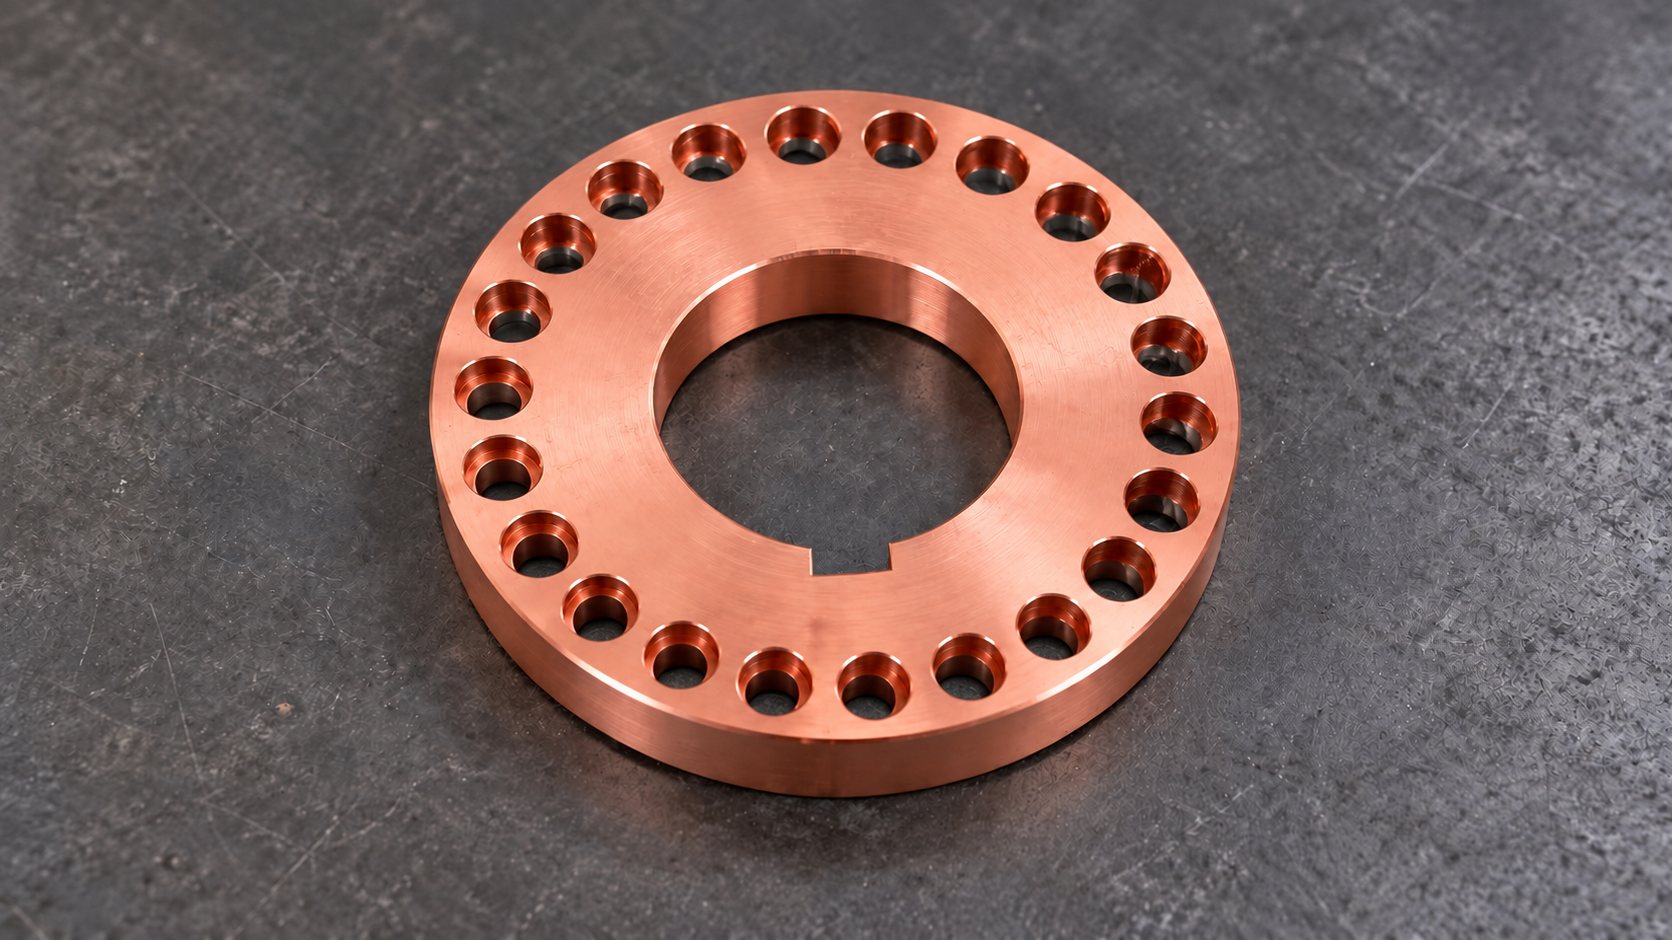
SIPENG CNC developed a drilling and chamfering solution for copper end rings used in submersible pump motor rotors, combining CNC machining, through-spindle coolant and dedicated fixtures to address chip wrapping, manual clamping and repetitive handling.
Read case study →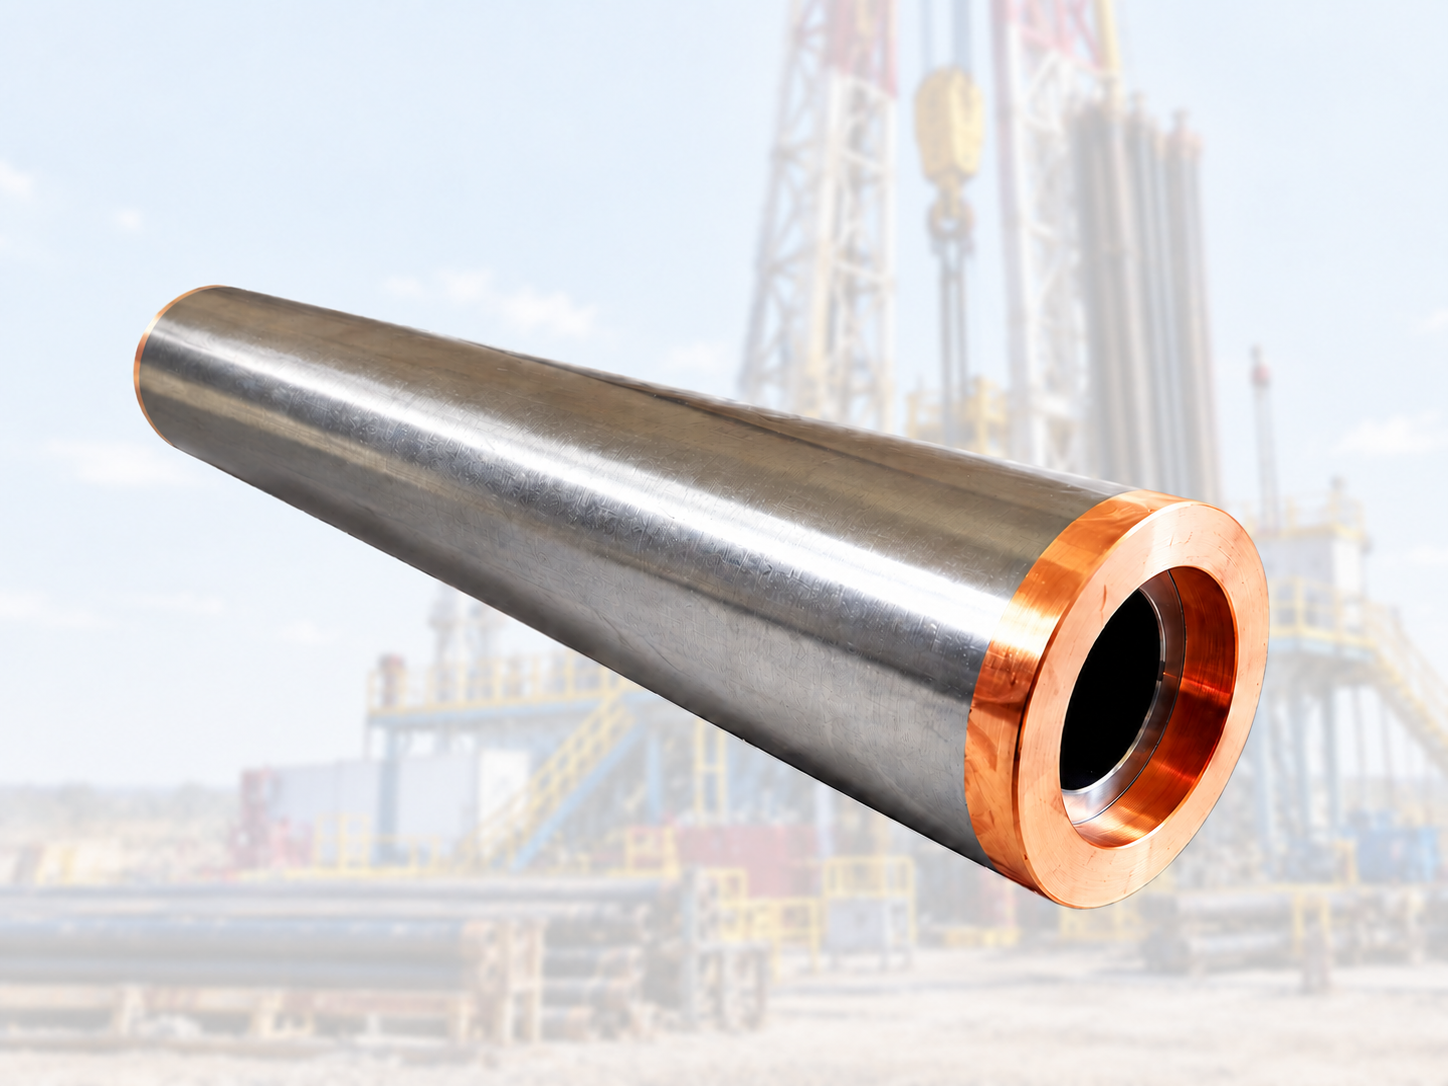
To address issues such as tool switching, repeated alignment, and handling-induced damage during the machining of the outer diameter of submersible pump motor rotor assemblies, this case study reconfigures the machine tool, internal bore clamping method, and workpiece handling process, enabling continuous external turning in a single setup while protecting the machined surfaces.
Read case study →
A pipe fitting manufacturer replaced scattered manual lathes with a cell of CNC lathes fed by bar feeders. Process planning, tooling packages, part programs and operator training were delivered with the machines, so fitting blanks now move through the cell on a fixed, repeatable route.
Read case study →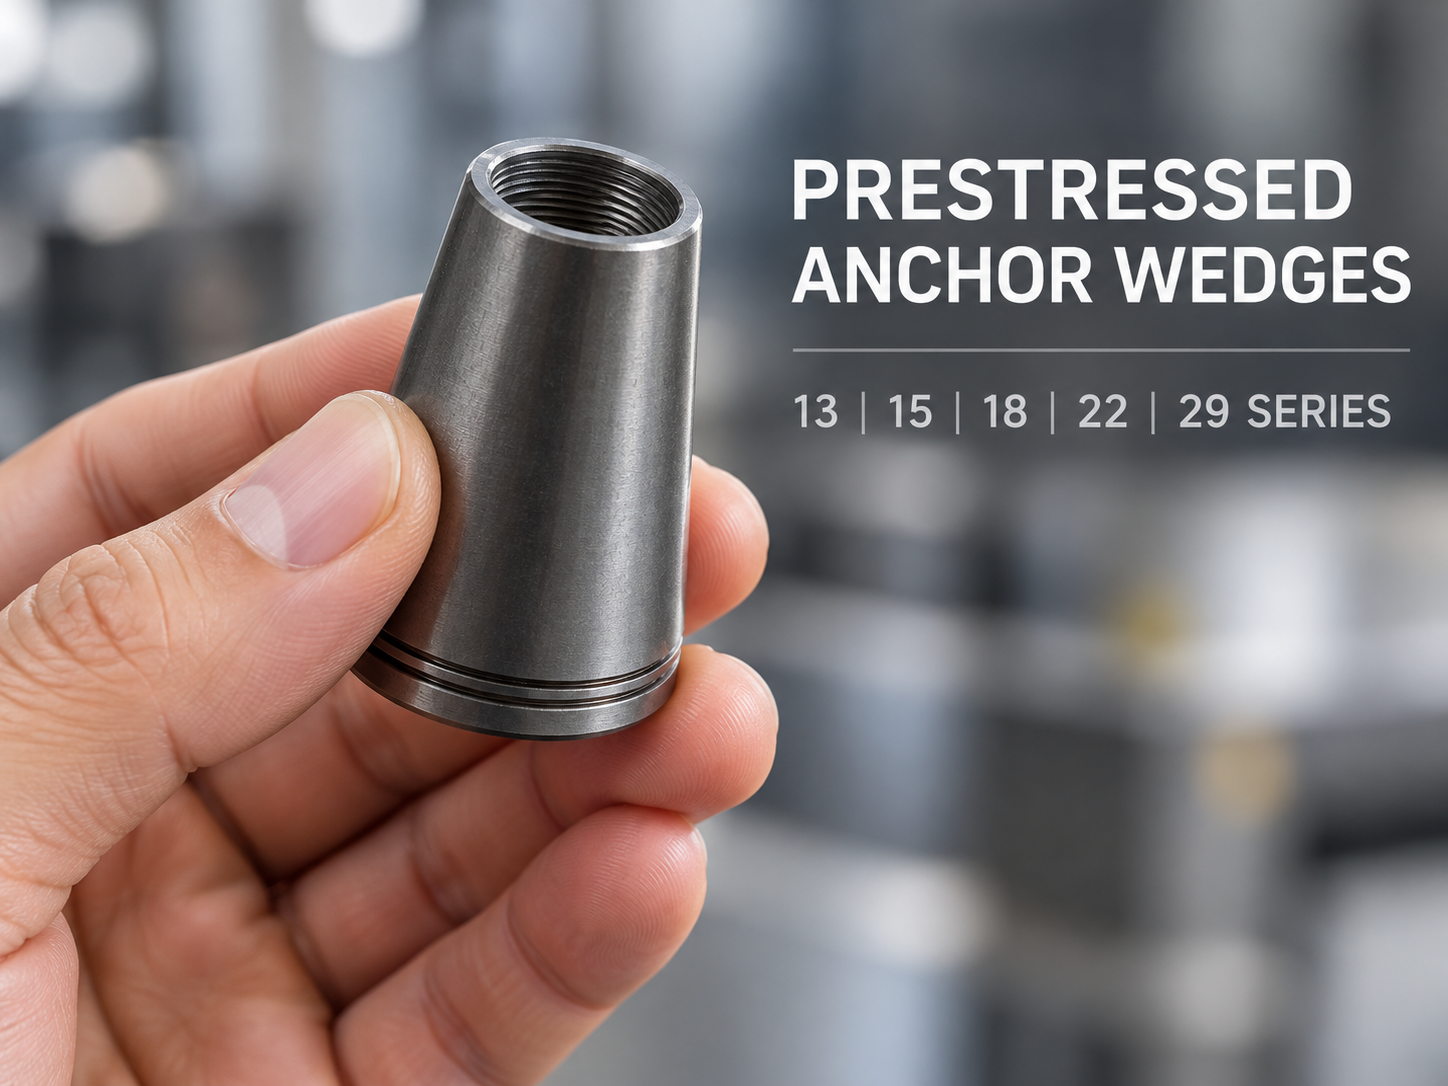
An elevating feeder and dual-channel CNC lathe were added to automate handling for prestressed anchorage wedge turning. The customer reports about 20 seconds per part in the original process and about 14 seconds in the new process; the time scope and production results should be verified on a consistent basis.
Read case study →